Sizing Wrapper Fleets From Kitchen Mass Flow
Confectionery process equipment is rated in kilograms per hour (kg/h), whereas single-piece wrappers are rated in pieces per minute (PPM). Part of candy wrapper sizing and selection and candy wrapping film and sealing specs, bridging that unit gap accurately prevents either starving expensive wrappers or backing up a live cooking line.
Formula: Required Fleet PPM = [(Line kg/h × 1,000) ÷ (60 × Single Piece g)] ÷ 0.85 Effective Availability.
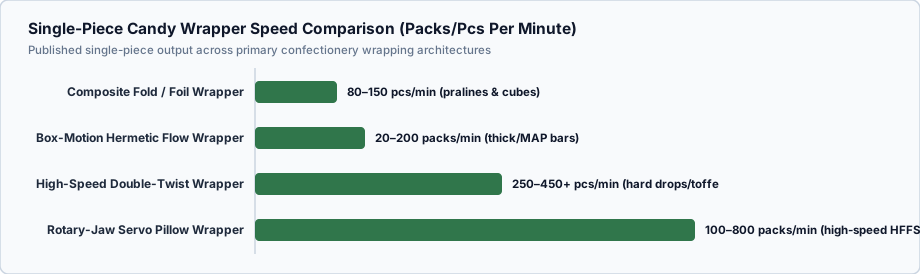
Reference Conversion Table: kg/h to Wrapper Fleet
Use the pre-calculated engineering matrix below (includes 15% surge/splice margin):
| Process Line Output | 3.5 g Hard Drop | 6.0 g Toffee Chew | 15 g Mini Bar | 40 g Countline Bar |
|---|---|---|---|---|
| 100 kg/h | 560 PPM (2× Twist or 1× Mini HFFS) | 327 PPM (1–2× Twist/Fold) | 131 PPM (1× 350 HFFS) | 49 PPM (1× 350 HFFS) |
| 250 kg/h | 1,401 PPM (4× Twist or 2× Mini HFFS) | 817 PPM (3× Twist or 2× HFFS) | 327 PPM (2× 350 HFFS) | 123 PPM (1× Cold-Seal HFFS) |
| 500 kg/h | 2,801 PPM (7× Twist or 4× Mini HFFS) | 1,634 PPM (5× Twist or 3× HFFS) | 654 PPM (2–3× High-Speed HFFS) | 245 PPM (1–2× Cold-Seal HFFS) |
| 800 kg/h | 4,482 PPM (11× Twist or 6× Mini HFFS) | 2,614 PPM (7–8× Twist) | 1,046 PPM (3–4× High-Speed HFFS) | 392 PPM (2× Cold-Seal HFFS) |
Pair machine counts with film consumption math on our flow-wrap film width chart.
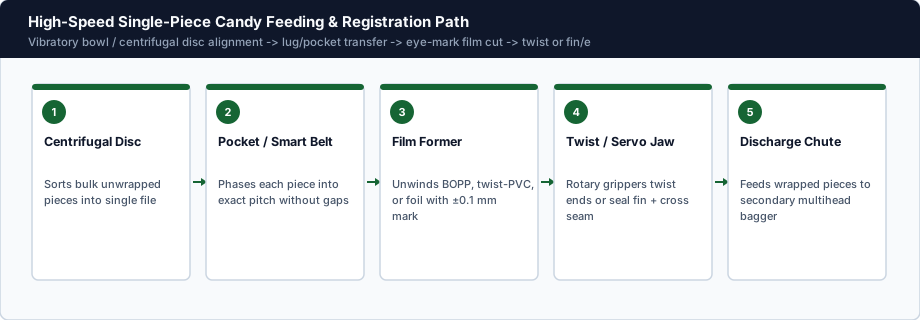
High-Speed Wrapping Engineering Notes
- Why Auto-Splicers Cut Machine Count: Adding dual-reel automatic splicers raises single-wrapper availability from ~83% to ~95%, often saving an entire wrapper leg on large lines.
- Cut-and-Wrap Rope Speed Limit: Rope-fed chew machines are bounded by linear rope stability (~25–45 m/min) as well as cut frequency.
- Secondary Bagger Pairing: Divide total wrapped PPM by pieces-per-bag to size your downstream multihead VFFS bagger (e.g., 1,200 PPM ÷ 30 pcs/bag = 40 bags/min).
Verify Your Fleet Count Before Floor Layout
Send your kitchen output (kg/h), piece weight range, and floor space to balance speed per head versus N+1 redundancy.
Submit your figures via our Project Brief.
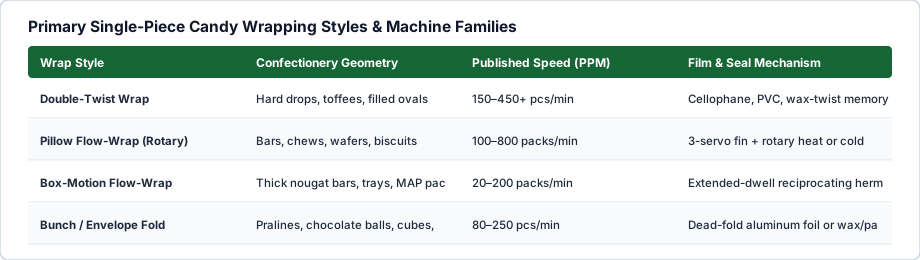
Explore related single-piece systems in Candy Wrapping Machines, Film & Sealing Specs, or submit your piece dimensions via Project Brief.
Related Specifications
Further Reference
Request Project Configuration Review
Share layout constraints, architectural drawings, or throughput targets with Candy Wrapping Machine Technical Group.
Discuss My Wrapper Specs